How to Calculate Injection Molding Mold Cost in 2026?
Calculating injection molding mold cost in 2026 requires more than checking a supplier’s first quotation. The visible price may cover steel, machining, assembly, and basic testing. It may exclude design revisions, mold trials, texture, freight, maintenance, or production changes. That gap can quietly damage a project budget.
John Bozzelli, a respected injection molding consultant, has emphasized, “The mold is the heart of the molding process.” His point remains practical. A mold with polished cavities, balanced cooling channels, and reliable ejection can reduce defects and downtime. A cheaper mold may create flash, short shots, uneven shrinkage, or difficult part removal. Those problems cost money after delivery.
This guide explains how to estimate injection molding mold cost with greater control. It examines part geometry, cavity count, mold steel, tooling standards, surface finish, hot runner systems, tolerances, and expected production volume. A small two-plate mold for a simple cap may cost far less than a complex multi-cavity mold with slides and unscrewing features. Details matter.
Prices also vary by region, supplier capacity, steel selection, and delivery schedule. In 2026, automation, energy expenses, software, and supply-chain conditions may influence quotations. Not every estimate will be perfectly predictable. That is worth admitting. A spreadsheet can reveal assumptions, but it cannot replace a design review with an experienced toolmaker.
The goal is not finding the lowest number. It is finding a mold that performs consistently, survives its planned cycles, and supports the product’s real production needs.
What Determines Injection Molding Mold Cost in 2026?
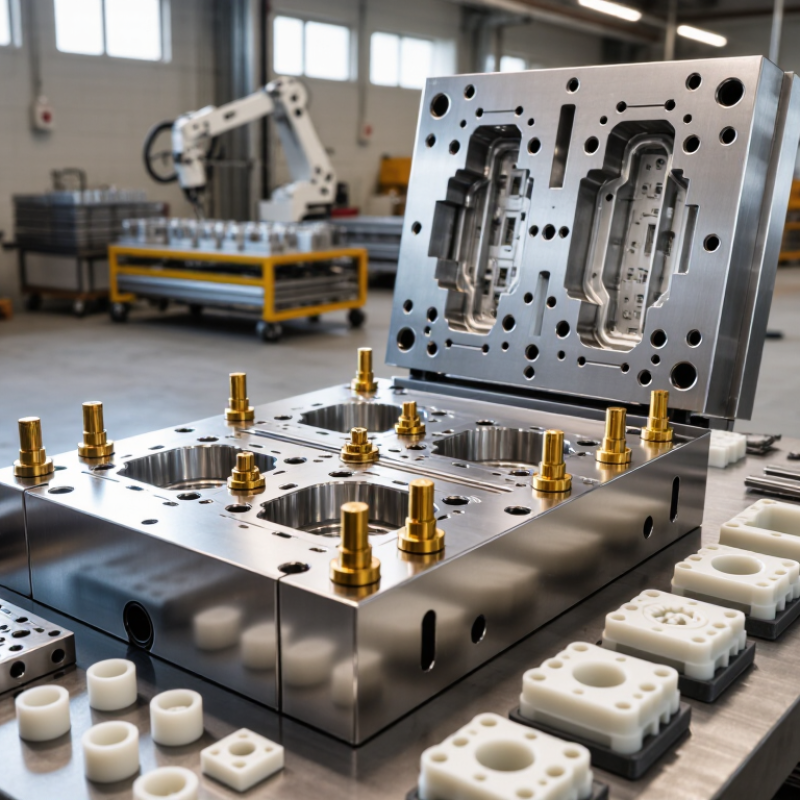
Injection molding mold cost in 2026 depends less on the plastic price than on tooling complexity.
A single-cavity mold with a flat parting line may cost about $3,000–$10,000.
Multi-cavity tooling, complex slides, lifters, or hot runners can exceed $50,000. These ranges vary by region and specification, so they are planning figures, not promises.
Mold steel, cavity count, surface finish, tolerances, cooling design, and expected shot volume strongly influence the quote.
A polished medical enclosure needs tighter inspection than a simple storage cap. Thin walls may require better cooling and higher machining accuracy.
PlasticsEurope reported global plastics production of 413.8 million tonnes in 2023, showing the scale of demand.
Grand View Research also projects continued growth in injection-molded plastics through 2030.
Higher production volumes can justify more cavities, but they increase upfront tooling costs.
Tool life matters too.
A hardened-steel mold usually costs more initially, yet it may reduce replacement risk.
Maintenance, spare inserts, sampling, and mold trials should appear in the budget.
They are often missed.
Tips:
Ask for a cavity layout, steel grade, cycle-time estimate, and maintenance plan.
Request separate prices for tooling, samples, modifications, and production.
Compare total cost per part, not only the mold invoice.
A cheaper mold can become expensive after repeated repairs.
Engineers should also challenge unnecessary tolerances; this is where many estimates quietly grow.
How to Estimate Material, Design, and Manufacturing Expenses
Estimating injection molding mold cost in 2026 starts with a clear part definition.
Record resin type, annual volume, tolerances, surface finish, and expected tool life. These details influence steel choice, cavity count, cooling layout, and maintenance allowances. A simple polypropylene housing may need a single-cavity aluminum tool for limited trials. A glass-filled engineering part usually demands hardened steel and stronger wear protection. Small details matter.
Design expenses begin before steel is cut.
A mold engineer reviews wall thickness, draft angles, ribs, bosses, parting lines, and ejection marks. Complex slides, lifters, unscrewing features, or hot-runner systems add machining and testing time. Request a 3D mold-flow review when weld lines or warpage could affect assembly. It costs money, but correcting a poor gate after machining costs more. I have seen early estimates miss electrode work and manual polishing. That mistake makes a low quote look reliable.
Manufacturing cost includes steel preparation, CNC machining, electrical discharge machining, grinding, polishing, assembly, and trial shots.
Ask for each item as a separate line in the quotation. Compare machining hours, inspection standards, sampling quantities, and revision allowances. Freight, packaging, spare inserts, and future repairs also deserve attention. No estimate is perfect. Material prices can change, and design revisions often arrive late. Keep a practical contingency, but do not hide uncertainty inside one unexplained total. A useful estimate shows what is known, what is assumed, and what still needs verification.
How Mold Complexity and Cavity Count Affect the Total Price
How to Calculate Injection Molding Mold Cost in 2026?
Mold cost depends heavily on complexity and cavity count, not only mold size. A single-cavity mold may cost less initially, but it produces one part per cycle. Multi-cavity tooling costs more because it needs additional cavities, balanced runners, cooling channels, and precise alignment. More cavities also increase machining time and inspection requirements.
Keep this practical. A basic mold with simple geometry may cost several thousand dollars, while a complex mold can exceed tens of thousands. Deep ribs, undercuts, sliding cores, lifters, textured surfaces, and tight tolerances each add expense. For example, an undercut may require a side action, which adds components and maintenance points. I have seen early estimates fail because they ignored cooling design. Poor cooling can lengthen cycle times and reduce the expected savings from extra cavities.
A useful estimate combines mold base, cavity machining, core steel, ejection, cooling, surface treatment, testing, and engineering labor. Cavity count affects more than the purchase price. It can reduce the cost per part when production volume is high, but it may increase setup difficulty and repair costs. Product size matters too. Eight small cavities may fit efficiently, while four large cavities could require a much larger mold base. The best choice depends on annual demand, target cycle time, material, and acceptable maintenance risk. Do not overbuild too early. That mistake is common.
How to Calculate Injection Molding Mold Cost in 2026? - How Mold Complexity and Cavity Count Affect the Total Price
Indicative 2026 injection mold cost ranges in USD. The estimates are intended for early-stage budgeting and assume a production mold using standard tool steels, normal dimensional tolerances, and conventional injection molding processes.
| Mold Complexity |
Typical Part Characteristics |
1 Cavity
Estimated Cost |
2 Cavities
Estimated Cost |
4 Cavities
Estimated Cost |
8 Cavities
Estimated Cost |
Typical Build Time |
Indicative Mold Life |
| Simple |
Open-and-shut part, limited texture, no side actions, standard tolerances |
$8,000–$18,000 |
$12,000–$25,000 |
$18,000–$38,000 |
$30,000–$60,000 |
4–7 weeks |
100,000–300,000 cycles |
| Medium |
Moderate ribs, multiple inserts, molded texture, tighter tolerances, limited sliders |
$15,000–$32,000 |
$22,000–$45,000 |
$35,000–$70,000 |
$55,000–$110,000 |
6–10 weeks |
300,000–700,000 cycles |
| Complex |
Deep cores, thin walls, lifters, multiple sliders, high-precision features, complex cooling |
$30,000–$65,000 |
$45,000–$90,000 |
$70,000–$140,000 |
$110,000–$220,000 |
10–16 weeks |
500,000–1,000,000 cycles |
| Highly Complex |
Unscrewing mechanisms, collapsible cores, hot-runner systems, optical surfaces, very tight tolerances |
$55,000–$120,000 |
$80,000–$170,000 |
$130,000–$280,000 |
$220,000–$450,000 |
14–24 weeks |
500,000–1,500,000 cycles |
How the estimate is calculated:
Estimated Mold Cost = Base Mold Cost + Cavity Adders + Ejection System Cost + Core/Slider Mechanism Cost + Runner System Cost + Cooling and Finish Cost + Engineering and Validation Cost
- Cavity count: More cavities increase the cost of steel, machining, polishing, alignment, cooling channels, and validation. The cost per cavity usually decreases as cavity count rises, but the total mold price increases.
- Complexity: Sliders, lifters, collapsible cores, unscrewing mechanisms, thin-wall sections, undercuts, and high-precision surfaces can substantially increase machining and assembly costs.
- Runner system: A cold-runner mold generally has a lower initial cost, while a hot-runner mold commonly adds approximately $8,000–$40,000 or more depending on the number of drops, valve gates, temperature zones, and control requirements.
- Material and finish: Hardened steel, mirror polishing, premium textures, corrosion-resistant steel, and special coatings can increase the tooling budget by approximately 10%–35% compared with a standard mold specification.
- Excluded items: The ranges normally exclude production parts, resin, freight, import duties, mold modifications after approval, special inspection equipment, and machine-side automation.
- Important planning note: Actual pricing varies by part size, projected area, wall thickness, resin type, tolerance requirements, annual volume, mold life target, toolmaker location, and the required delivery schedule.
How to Calculate the Final Injection Mold Cost Step by Step
How to Calculate Injection Molding Mold Cost in 2026?
Calculate the final injection mold cost by separating every production stage. Start with the part drawing, resin type, monthly volume, and expected mold life. A small prototype mold may use aluminum, while high-volume production usually requires hardened steel. The material choice changes durability, machining time, and maintenance costs.
Estimate the base mold structure first. Add cavity numbers, core and cavity machining, inserts, cooling channels, ejector components, and the mold base.
Then include design engineering, CNC machining, electrical discharge machining, polishing, assembly, and dimensional inspection.
A simple single-cavity mold may cost between 3,000 and 8,000 dollars, but complex multi-cavity tooling can exceed 50,000 dollars.
Do not stop at the machining quote. Add trial molding, sample inspection, corrections, surface treatment, packaging, freight, and applicable taxes. The practical formula is: final cost equals tooling price plus testing, revisions, logistics, and taxes. Ask whether the quote includes steel certification and spare components. It matters.
A first estimate is rarely perfect. Small details can grow expensive.
For example, a deep rib may require special machining, while tight tolerances can increase inspection time.
An experienced mold engineer should review draft angles, wall thickness, parting lines, and cooling layout before approval. This review can prevent expensive modifications later, although it cannot remove every production risk. Recheck the estimate after the first mold trial.